

- Site Navigation -
How Cargo Tricycles Are Manufactured: Production Process
Author:duomi Date:2026-09-26 15:33:50 Hits:74
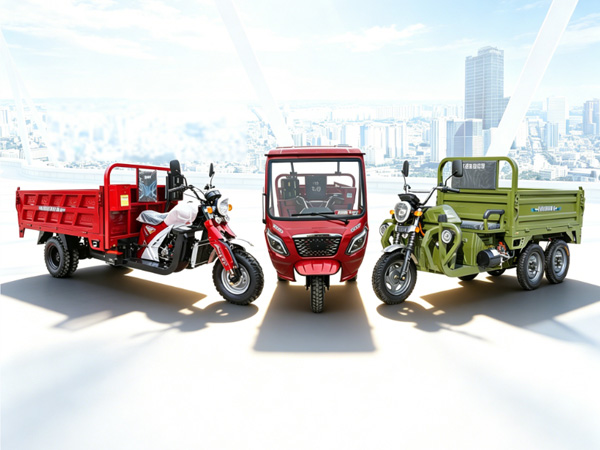
The vehicle that arrives in your fleet has passed through a series of manufacturing stages, each of which introduces quality variables that affect the final product's performance, durability, and safety. For B2B buyers who specify, procure, and operate cargo tricycles, understanding how these vehicles are manufactured is not an academic exercise—it is practical procurement intelligence. Knowing which processes a manufacturer controls in-house versus outsources, what testing they conduct at each stage, and how their quality management system catches defects before vehicles reach customers tells you more about what you will receive than any sales pitch.
Frame Design and Engineering: The Document That Guides Everything
Before any steel is cut, the manufacturing process begins with engineering. The frame geometry—tube diameters, wall thicknesses, joint angles, and overall dimensions—is designed to meet specific payload ratings, stability requirements, and ergonomic targets. Reputable manufacturers develop frames using CAD software that simulates stress distribution under rated load conditions, allowing structural engineers to optimize tube wall thickness at high-stress joints without over-engineering low-stress sections.
The critical design documents that govern the manufacturing process are the engineering drawings and bill of materials. Engineering drawings specify every tube cut length, bend angle, weld joint preparation, and fastener specification with tolerances. The bill of materials lists every component—from frame tubes and axle stock to bolts, bearings, and brake components—with part numbers, quantities, and approved supplier references. When a buyer evaluates a manufacturer, requesting samples of their engineering documentation and BOM structure gives a reliable indication of their engineering discipline. Manufacturers who cannot produce coherent, detailed engineering documentation are manufacturing by guesswork rather than design.
Steel Selection and Tube Procurement
The frame is the structural backbone of any cargo tricycle, and its material determines fatigue life, load rating, and corrosion resistance. Commercial-grade cargo tricycles are fabricated from mild carbon steel tubing—typically Q215 to Q235 grade in Chinese manufacturing standards, equivalent to ASTM A36 internationally. The key material parameters are tensile strength, yield strength, and wall thickness consistency.
Tube wall thickness tolerance has a direct impact on frame weight and structural integrity. Quality-focused manufacturers source tubing with wall thickness tolerance of ±5% or tighter, ensuring that every tube in every frame has consistent mechanical properties. Budget manufacturers may use tubing with ±15% or wider tolerance, meaning some tubes are meaningfully weaker than the engineering calculation assumes. For cargo tricycle frames intended for commercial use at 500–1,000 kg payload ratings, wall thickness of 2.0–2.5 mm for main frame tubes and 2.5–3.0 mm for high-stress sections is the standard specification. Tube that is visibly thin or varies noticeably in thickness between sections is a quality indicator that should raise concerns.
Surface condition of the incoming tube matters too. Mill scale—a hard iron oxide layer that forms on hot-rolled steel—must be removed before welding, either by sandblasting or acid pickling. Frames fabricated from tube with mill scale intact produce welds with poor fusion at the scale inclusions, dramatically reducing weld strength. A quality manufacturer includes surface preparation as a documented step in their incoming material inspection.
Frame Fabrication: Cutting, Bending, and Preparation
The fabrication stage transforms raw steel tube into the structural components that will be welded into a complete frame. The first operation is cutting—tube is cut to length on band saws or automated cutting machines that produce square, clean cuts without heat-affected zones or excessive burr. Precision-cut ends are critical: a cut that is even 2–3 degrees off-square creates cumulative alignment problems across a multi-tube frame joint.
Bending is required for tubes that form the curved sections of the head tube, seat tube, and rear triangle. Bending is performed on mandrel tube benders that support the tube interior during the bend, preventing the ovalization and wall thinning that occur with simple compression bending. The quality of the bend is verified by checking the cross-section at the bend apex—excessive ovalization (more than 10% of tube diameter) or visible wall thinning indicates improper bending technique or incorrect die selection. After bending, tube ends are prepared for welding: the inner surfaces of tubes that will be joined are cleaned, and the joint geometry is prepared according to the welding procedure—typically a 45-degree bevel on thicker tubes to ensure full penetration weld fusion.
Welding: The Process That Determines Frame Life
Welding is the most technically demanding and consequential manufacturing operation in cargo tricycle production. The frame's fatigue life under commercial loading depends almost entirely on weld quality, and weld failures at high-stress joints are the most common cause of premature frame failures in budget vehicles.
Frame welding for cargo tricycles is performed using gas metal arc welding (GMAW, commonly MIG/MAG welding) for its combination of weld quality, speed, and accessibility. The process uses a continuous filler wire electrode and a shielding gas—typically a mixed argon-CO₂ blend—that protects the weld pool from atmospheric contamination. The quality variables that affect weld strength are: weld joint preparation (bevel angle and fit-up tolerance), shielding gas purity and flow rate, wire feed speed and voltage settings matched to material thickness, welder skill and consistency, and post-weld inspection and non-destructive testing where required.
Reputable manufacturers use fixturing jigs that hold frame components in precise alignment during welding. Jig-fixtured welding ensures that every frame emerges from the welding station with consistent geometry—critical for subsequent assembly operations that depend on accurate frame dimensions. Frames welded without jigs rely on the individual welder's ability to hold alignment by eye, producing inconsistent geometry that complicates assembly and may introduce stress concentrations from misaligned joints.
After welding, the frame undergoes weld cleaning and inspection: removal of slag, spatter, and sharp weld toes that would concentrate stress; visual inspection for defects including porosity, incomplete fusion, and undercut; and measurement of critical dimensions against engineering tolerances. A quality manufacturer documents this inspection and rejects frames that do not meet dimensional tolerances.
Surface Treatment and Corrosion Protection
The finished frame must be protected against corrosion before assembly. In service environments—rain, road salt, soil, fertilizer, industrial chemicals—the frame surface is exposed to conditions that attack bare steel aggressively. A cargo tricycle without adequate corrosion protection develops rust at weld joints within 12–24 months, compromising frame strength and creating an unsafe condition.
The standard surface treatment process for commercial cargo tricycles is multi-stage pretreatment followed by powder coating. The pretreatment stages are: degreasing to remove mill oil, cutting fluid, and handling contaminants; iron phosphate conversion coating to create a surface that the powder coating bonds to chemically; and chromic acid rinse or sealing rinse to improve corrosion resistance of the phosphate layer. After pretreatment, the frame is dried in a bake oven to remove all moisture before powder coat application.
Powder coating is applied electrostatically—the powder particles are charged and attracted to the grounded frame, creating an even coating that is then cured in a 180–200 degree Celsius oven. The result is a uniform, adherent coating of 60–100 microns thickness that provides excellent stone-chip resistance and chemical resistance compared to conventional liquid paint. For vehicles intended for marine, coastal, or industrial chemical environments, additional measures such as hot-dip galvanizing or marine-grade powder coating are specified as premium options.
Component Assembly and Integration
With the frame fabricated, treated, and inspected, the vehicle moves to the assembly stage. Assembly follows a structured sequence: wheels and hubs are installed first, establishing the vehicle's wheelbase and track dimensions; the drivetrain (chain, sprockets, and rear axle) is installed and tensioned; the steering assembly (headset, handlebar, and stem) is installed and adjusted; the brake system is installed and bled; for electric models, the motor, controller, battery mount, and wiring harness are installed and connected; the cargo bed is mounted; and finally, the seat, controls, and lighting system are installed.
The critical assembly operations that affect safety and durability are: wheel bearing preload adjustment (bearing play must be eliminated without preloading to the point of binding), chain tension and alignment (a misaligned chain wears rapidly and can jump sprocket teeth), brake cable adjustment (brake lever travel to full braking force should be within one-third of lever travel), and electrical connector seating (all connectors must be fully seated and secured with locking clips to prevent vibration-induced disconnection).
Testing and Quality Control Before Dispatch
No cargo tricycle should leave a manufacturer's facility without passing through a structured testing protocol. The minimum acceptable testing sequence includes: visual inspection of the complete vehicle against the assembly checklist, wheel bearing play check, chain tension and alignment check, brake function test (full braking force within one-third lever travel), parking brake hold test on a 12-degree slope, lighting and electrical function test, and a ridden test of minimum 2 km under load covering acceleration, braking, cornering, and stability.
Quality-focused manufacturers conduct batch testing of frame samples—destructive fatigue testing of production frames to verify that the actual fatigue life meets or exceeds the design specification. This is particularly important for manufacturers supplying cargo tricycles for high-utilization commercial fleets, where frames accumulate thousands of loading cycles per year. Buyers sourcing from manufacturers who publish frame fatigue test data have a concrete basis for confidence in frame durability that buyers from non-testing manufacturers must take on faith.
Frequently Asked Questions
What is the difference between a manufacturer that welds frames in-house and one that outsources frame production?
In-house frame welding allows the manufacturer to control weld quality, jig-fixturing, and inspection processes directly. Outsourced frames introduce a quality interface between the welding supplier and the assembly facility, and the level of quality control at the welding stage may be unknown to the final assembler. Buyers should ask whether the manufacturer welds frames in-house and, if outsourced, request documentation of the welding supplier's quality certifications.
How does the manufacturing process affect the payload rating of a cargo tricycle?
The payload rating is determined by frame structural engineering (tube wall thickness and geometry), confirmed by testing, and must be supported by the component specifications throughout the vehicle—axle, bearings, wheels, brakes, and suspension all have load ratings that must meet or exceed the frame rating. A vehicle that claims a high payload rating but specifies undersized components in those critical systems is engineered optimistically at best and dangerously at worst.
What quality certifications should I look for in a cargo tricycle manufacturer?
ISO 9001:2015 quality management system certification is the baseline standard for a quality-focused manufacturer. For frame production, IATF 16949 (automotive quality management) indicates rigorous process control. Request copies of the manufacturer's current certifications and verify them with the issuing certification body. Also request frame fatigue test data, assembly inspection records, and a sample of their engineering documentation to assess engineering discipline directly.
How can I verify manufacturing quality if I am sourcing from overseas?
Request a pre-shipment inspection by an independent third-party inspection company (SGS, Bureau Veritas, and Intertek all offer this service). Commission a sample order of 3–5 units for thorough inspection and testing before committing to a full container order. Conduct video factory audits or request a live video walkthrough of the production line. Ask for references from existing customers in your market or application area.
Conclusion
Understanding how cargo tricycles are manufactured gives B2B buyers the evaluative framework they need to distinguish between suppliers who engineer for commercial durability and those who manufacture to a price point. The key differentiators are: in-house engineering capability with documented CAD design and BOM management, controlled welding with jig-fixturing and post-weld inspection, proper multi-stage surface preparation and powder coating, structured assembly with critical dimension verification, and batch fatigue testing that confirms frame life meets design specifications. Buyers who apply these criteria in their supplier evaluation process consistently receive vehicles that perform reliably in commercial service, with lower failure rates and longer service life than those sourced without manufacturing process due diligence.
References
ASM International, "Welding Processes and Technology," ASM Handbook Volume 6, 2nd Edition, 2017.
Bhadeshia, H.K.D.H. and Honeycombe, R.W.K., "Steels: Microstructure and Properties," Elsevier, 4th Edition, 2017.
Kalpakjian, S. and Schmid, S.R., "Manufacturing Engineering and Technology," Pearson, 7th Edition, 2013.
European Committee for Standardization, "EN 17860-1: Cycles — Safety Requirements for Cargo Bicycles," CEN, 2023.
International Organization for Standardization, "ISO 9001:2015 — Quality Management Systems," ISO, 2015.
Contact Us
Tel:8615713172715 / 8619061777149
WeChat:8615713172715 / 8619061777149
E-mail:942778859@qq.com
Url:https://www.duomitricycle.com