

- Site Navigation -
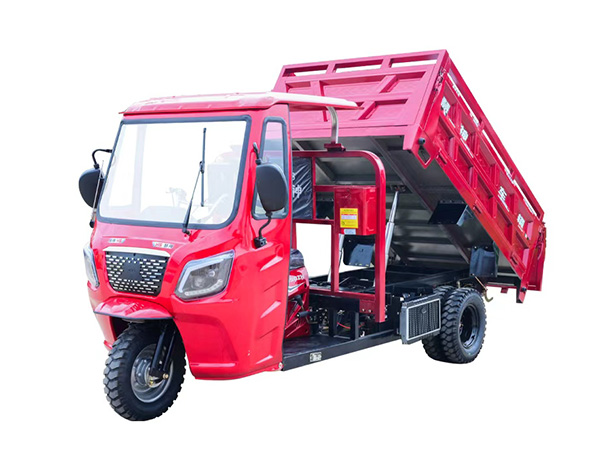
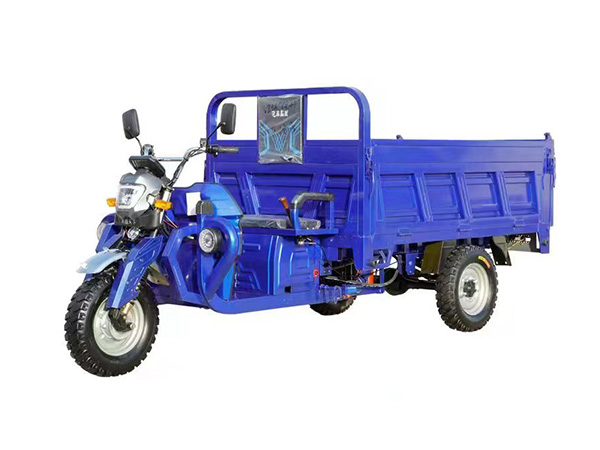
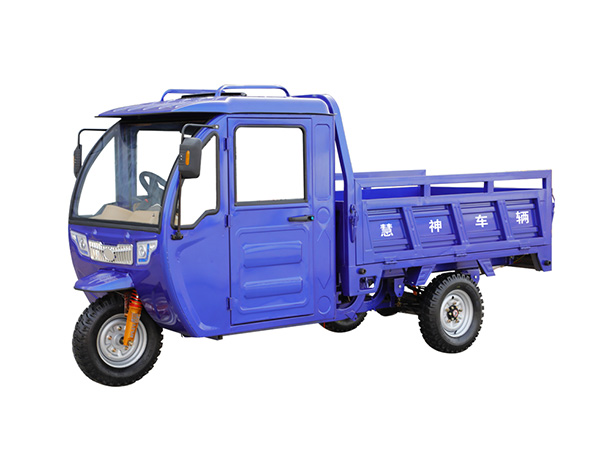
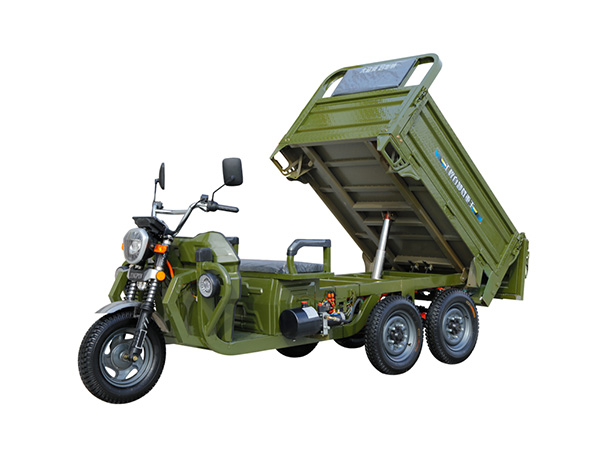
Structural Frame Design of Cargo Tricycles: Engineering Guide
Author:duomi Date:2026-09-17 13:21:49 Hits:101
The frame of a cargo tricycle is more than a structural skeleton—it is the primary determinant of every performance characteristic that matters in commercial service. Payload rating, stability, fatigue life, ride quality, and corrosion resistance are all fundamentally shaped by decisions made during frame design: what steel to use, what tube sizes and wall thicknesses to specify, how to arrange the tube geometry, where to place welds, and how to protect the finished structure from corrosion. For engineers, technical buyers, and product developers evaluating cargo tricycle frame design, understanding these relationships is essential to distinguishing between vehicles engineered for commercial durability and those that will develop problems within months of entering service.
Material Selection: Why Steel Remains the Standard
Cargo tricycle frames are almost universally fabricated from steel, and for good engineering reasons. Steel offers the combination of high yield strength, good fatigue resistance, ease of fabrication through welding and bending, and cost-effectiveness that no alternative material matches at this price and performance point. Aluminum alloy frames are lighter but cost 2–3× more for equivalent strength in this application, and aluminum's fatigue behavior under variable amplitude loading is less forgiving than steel's. Composite frames are not economically viable for the price points that commercial cargo tricycle markets support.
The steel grades used in cargo tricycle frame design are mild carbon steels in the 250–350 MPa yield strength range. Chinese standard Q215–Q235 grade steel (equivalent to ASTM A36, with Q235 being the higher strength variant) is the industry standard for commercial-grade frames. For heavy-duty frames rated above 800 kg payload, Q345 (16Mn, equivalent to ASTM A572 Grade 50) with its 345 MPa yield strength provides a meaningful increase in strength-to-weight ratio, though at a higher cost. The key material parameters that affect frame performance are: yield strength (determines the load at which permanent deformation begins), tensile strength (the load at which the material fractures), elongation at break (a measure of ductility—higher elongation means more forgiving behavior under overload), and consistent wall thickness tolerance (variation above ±5% affects structural predictability).
Tube Geometry and Sizing: Matching Section to Stress
The geometry of the frame members—their diameter, wall thickness, cross-sectional shape, and orientation—determines how efficiently the material resists the loads applied to it. In cargo tricycle frame design, loads come from multiple directions: vertical loads from the weight of the vehicle, cargo, and rider; longitudinal loads from acceleration and braking; lateral loads from cornering forces; and torsional loads from uneven road surfaces that twist the frame.
Circular steel tube is the dominant cross-section in cargo tricycle frames because it provides equal bending stiffness in all directions, is easy to join with good weld penetration, and bends cleanly without section collapse. The tube diameter and wall thickness are sized based on the stress analysis for each member. High-stress members—head tube, main down tube, rear dropout sections—use larger diameter tube with thicker walls. Lower-stress members—secondary bracing tubes—use smaller diameter and thinner walls. This graduated sizing is more efficient than using uniform tube throughout: it reduces weight and cost while maintaining adequate strength where it is needed.
Butted tubes—tubes with thicker walls at the ends than in the middle—optimize this approach further. The tube ends are the high-stress regions where tubes are joined by welding; the mid-span of the tube experiences lower bending stress and can use thinner walls. Butted tubes reduce weight 10–15% compared to constant-wall tube at equivalent fatigue life, but add cost and require more precise bending technique. They are standard specification in frames designed for high-utilization commercial fleets but optional in budget models.
Load Path Analysis: How Forces Flow Through the Frame
A well-designed cargo tricycle frame routes loads from the point of application through the frame structure to the wheels and ground in the most efficient path possible. Understanding this load path is essential to evaluating whether a frame design is appropriate for its intended payload and application.
The primary load path for vertical loads begins at the cargo bed mounting points, flows through the main frame tubes (down tube, seat tube, and chain stays) to the bottom bracket and rear axle, and from there through the wheels to the ground. The chain stays and seat stays transfer the cargo load to the rear axle; the main tubes transfer it to the head tube and front fork. Lateral loads from cornering are resisted by the triangulated geometry of the rear triangle—three tubes forming a structural truss that resists sideways deflection—and by the head tube assembly, which transfers cornering forces to the front wheel.
The quality of a frame's load path design shows up in how it distributes stress concentrations. Sharp corners, abrupt section changes, and poorly positioned welds all create localized stress peaks that accelerate fatigue failure. The engineering principle that governs good cargo tricycle frame design is gradual load transfer: transitions between members should be smooth and continuous, welds should be placed at low-stress locations, and gusset plates or reinforcement should be used at junctions where multiple load paths converge. A frame that shows evidence of abrupt geometry or excessive weld density at joint intersections is likely to develop fatigue cracks at those locations under commercial loading.
Frame Geometry: Stability, Handling, and Ergonomics
Beyond structural load-bearing, cargo tricycle frame design must balance stability, handling, and operator ergonomics—three objectives that sometimes conflict and must be resolved through engineering compromise.
Wheelbase—the distance between front and rear axle centers—affects both stability and maneuverability. A longer wheelbase provides more stable straight-line tracking and reduces the pitching motion from road surface irregularities, but requires more space to turn. A shorter wheelbase is more maneuverable in tight spaces but transmits more road shock to the frame and cargo. Commercial cargo tricycles typically use wheelbases of 1,400–1,800 mm, with the longer end of this range preferred for vehicles with larger cargo beds and higher payload ratings.
Rear track width—the distance between the centers of the two rear wheels—determines the width of the stability triangle. A wider rear track increases lateral stability but makes the vehicle harder to fit through standard doorways and narrow aisles. The standard rear track for commercial cargo tricycles is 850–1,100 mm, with the wider end preferred for high-payload vehicles. The head tube angle—the angle at which the front fork attaches to the frame—affects steering responsiveness and high-speed stability. A steeper head angle (closer to vertical) produces quick, light steering suitable for urban delivery; a slacker angle (more reclined) provides more stable straight-line tracking at the cost of slower steering response.
The cargo bed mounting height—the distance from the ground to the cargo bed floor—affects both stability and loading ergonomics. A lower bed is more stable (lower center of gravity for the load) and easier to load manually, but may interfere with the rear wheel's suspension travel or ground clearance. A higher bed reduces interference but raises the load's center of gravity and increases loading effort. The design compromise for most cargo tricycles sets the bed floor at 300–400 mm from ground—low enough for stable loaded operation and manual loading, high enough for adequate wheel and ground clearance.
Weld Joint Design: Where Frames Fail
The welds in a cargo tricycle frame are simultaneously its strongest and its most vulnerable elements. A properly made weld provides a joint as strong as the base material—the stress has no reason to prefer the weld over the tube. But welds are also stress concentration points: the heat-affected zone adjacent to the weld experiences changes in grain structure and hardness that can reduce fatigue resistance relative to the base material.
The cargo tricycle frame design must account for this by placing welds in locations where stress is low relative to the surrounding material. Welds at the tips of tubes (toe-of-weld locations) are high-stress areas where fatigue cracks most commonly initiate. Welds placed in the mid-span of tubes, away from geometric discontinuities, are lower-stress and less prone to fatigue. Frame designers who understand this principle locate their critical welds away from high-stress concentrations; those who do not create frames with weld-related fatigue vulnerabilities that may not become apparent for 12–18 months of commercial use.
The weld joint preparation—the geometry of the joint before welding—is also part of frame design. For tube thicknesses above 2 mm, a beveled joint preparation allows the weld to penetrate fully through the tube wall, creating a full-penetration weld. For thinner tubes, a simple butt joint with adequate gap for the weld to bridge is sufficient. Full-penetration welds at high-stress joints are a quality indicator; single-sided fillet welds at critical joints are a risk factor for premature failure.
Fatigue Design and Safety Factors
A cargo tricycle frame in commercial service experiences variable amplitude loading—thousands of cycles of loading and unloading at different magnitudes as the vehicle travels over rough surfaces, accelerates, brakes, and carries varying loads. This variable loading causes fatigue: microcracks that initiate at stress concentrations (often weld toes) and grow incrementally under repeated loading until the remaining cross-section can no longer carry the load.
The fatigue life of a frame is calculated by analyzing the expected load spectrum, determining the stress ranges at each critical location, and applying a fatigue criterion (such as Miner's rule or a fatigue design code) to estimate the number of cycles to crack initiation. A conservative safety factor is applied to ensure the calculated fatigue life exceeds the design service life target by a margin that accounts for load variability and material property variation. Industry practice for commercial vehicle frames is to design for a minimum fatigue life of 2–3× the design service life, with a minimum safety factor of 2.0 on yield strength.
Buyers can evaluate a manufacturer's approach to fatigue design by requesting frame fatigue test data from prototype or production samples. The test should show the number of cycles to failure at a specified load amplitude—and the frame should exceed its design fatigue life target before failing. A manufacturer who cannot provide this data is not designing to fatigue requirements; they are building frames that may or may not survive the intended service life.
Corrosion Protection as Part of Frame Design
Cargo tricycle frame design must account for the service environment. Steel frames operating in wet, humid, coastal, or industrial chemical environments face ongoing corrosion attack that can reduce frame cross-section and compromise structural integrity. Corrosion protection is not an afterthought applied after design—it is a design consideration that affects material selection, joint geometry, and surface treatment specification.
Design decisions that affect corrosion performance include: avoiding crevices and moisture traps where water pools and accelerates corrosion, using compatible metals in any dissimilar metal joints to minimize galvanic corrosion, specifying adequate wall thickness to allow for corrosion margin over the design service life (typically 0.5–1.0 mm additional wall thickness as a corrosion allowance for uncoated steel), and designing surface treatment access so that pretreatment chemicals can reach all surfaces—including the interior of tubes that would otherwise trap moisture.
Frequently Asked Questions
What steel grade is appropriate for a heavy-duty cargo tricycle frame?
For cargo tricycle frames rated at 500–800 kg payload, Q235 grade mild carbon steel (equivalent to ASTM A36) with 2.0–2.5 mm wall thickness on main tubes is appropriate. For frames rated above 800 kg payload or intended for high-utilization commercial fleets, Q345 (ASTM A572 Grade 50) with butted main tubes provides a meaningful improvement in strength-to-weight ratio and fatigue life. Always verify the manufacturer's stated steel grade against the engineering documentation.
How does frame geometry affect the stability of a cargo tricycle?
Three geometry parameters dominate stability: rear track width (wider track = more lateral stability), cargo bed height (lower = lower center of gravity = more stable), and wheelbase (longer wheelbase = more stable straight-line tracking but less maneuverable). A well-designed cargo tricycle frame balances these parameters to achieve a stable platform for the rated payload without sacrificing the maneuverability required for the intended operating environment.
How are weld joints designed to prevent fatigue failures in cargo tricycle frames?
Fatigue-resistant weld joint design places welds in low-stress locations (mid-span of tubes rather than at tube ends), uses full-penetration welds at high-stress joints rather than single-sided fillets, avoids sharp weld toes through smooth transition grinding, and uses gusset plates or reinforcement at junctions where multiple load paths converge. A manufacturer who designs weld joint locations based on stress analysis is engineering for fatigue life; one who welds where it is convenient is building by guesswork.
What safety factor should a cargo tricycle frame be designed to?
Industry practice for commercial vehicle frames is a minimum safety factor of 2.0 on yield strength and a design fatigue life of 2–3× the target service life. A frame that meets these criteria should survive 6–10 years of commercial service under rated load conditions with proper maintenance. Frames designed to lower safety factors may be adequate for lighter loads but will fatigue prematurely under heavy commercial use.
Conclusion
The structural frame design of cargo tricycles determines the vehicle's payload capacity, stability, fatigue life, and safety margin throughout its commercial service. The key engineering disciplines that produce a quality frame are: appropriate steel grade selection with verified material properties, tube sizing matched to the stress analysis at each location, logical load path routing that avoids stress concentrations, fatigue-designed weld joint placement, adequate safety factors on both yield strength and fatigue life, and corrosion protection designed in from the start rather than added afterward. B2B buyers who understand these engineering principles and request documentation of each—material certificates, stress analysis data, weld joint specifications, fatigue test results, and surface treatment process—can evaluate frame quality objectively rather than relying on appearance, price, or marketing claims. A quality frame is an investment that delivers 8–12 years of reliable service; a compromised frame is a liability that reveals its limitations through failures.
References
ASM International, "Fatigue and Fracture: Understanding the Basics," ASM Handbook Volume 19, 2013.
Shigley, J.E. and Mischke, C.R., "Mechanical Engineering Design," McGraw-Hill, 11th Edition, 2020.
Bhadeshia, H.K.D.H. and Honeycombe, R.W.K., "Steels: Microstructure and Properties," Elsevier, 4th Edition, 2017.
Liu, J. and Zhu, P., "Structural Optimization of Bicycle Frame Geometry for Fatigue Life," Journal of Mechanical Design, vol. 137, no. 5, 2015.
European Committee for Standardization, "EN 17860-1: Cycles — Safety Requirements for Cargo Bicycles," CEN, 2023.
Contact Us
Tel:8615713172715 / 8619061777149
WeChat:8615713172715 / 8619061777149
E-mail:942778859@qq.com
Url:https://www.duomitricycle.com